Explore our flagship high-performance 3D printing filaments, manufactured under strict ISO9001 guidelines with inline dual-axis laser diameter monitoring.
Understanding the polymer formulation, particle dispersion chemistry, and optical layer-masking properties that make Marble PLA the premier choice for visual prototyping.
Marble PLA is synthesized by compounding premium virgin Polylactic Acid (PLA) polymer resin with precise concentrations of fine inorganic mineral particles and dark pigment speckles. This controlled masterbatch formulation ensures homogeneous dispersion along the entire extruded strand without causing localized density fluctuations.
Standard monochromatic PLA highlights FDM layer stepping under directional light. Marble PLA diffuses ambient light across its micro-textured surface, effectively masking z-axis layer lines. Prints emerge with an authentic matte stone aesthetic directly off the build plate, eliminating hundreds of hours of manual sanding and priming.
By optimizing the melt flow index (MFI) of the base resin, industrial Marble PLA maintains minimal volumetric shrinkage during glass-transition cooling. This dimensional stability allows architectural scale models and expansive decorative structures to print without corner warping or bed detachment.
From architectural firms in London to museum reproduction facilities in Tokyo, discover how global enterprises leverage Marble Filament PLA to transform production workflows.
Architectural design studios substitute labor-intensive foam and plaster modeling with direct FDM 3D printing in Marble PLA. Complex façade details, urban planning topographies, and interior room layouts can be produced overnight with accurate natural marble appearance.
Fine art conservators and cultural heritage institutions digitize classical statues and relief sculptures via 3D scanning, printing exact high-resolution physical replicas in Marble PLA for educational displays, tactile museum exhibits, and historical preservation.
Boutique home decor brands utilize Marble PLA to manufacture high-end lampshades, geometric plant pots, luxury cosmetic containers, and decorative interior accents. The material's subtle sheen elevates perceived product value in retail environments.
Commercial print farms operating automated printer arrays leverage Marble PLA's reliable extrusion properties to offer premium stone-finish print services. Higher retail price points per printed gram boost operational profitability compared to standard PLA printing.
Founded in 2011, Torwell Technologies Co., Ltd. leads the Asian extrusion market with high-volume automated lines, strict quality assurance, and unyielding material consistency.
Operating out of a modern 2,500 m² standardized clean factory floor, Torwell housing 6 fully automated high-speed extrusion lines dedicated to thermoplastic compounding. Our automated material feed systems ensure raw resin is continuously dried to sub-0.05% moisture levels before entering the screw extruder, preventing internal void formation and thermal degradation during melt processing.
To eliminate diameter drift—the primary root cause of nozzle clogging and under-extrusion—every millimeter of Torwell Marble Filament is monitored in real-time by inline dual-axis laser micrometers. Extrusion speeds automatically adjust within milliseconds to maintain a strict target diameter tolerance of ±0.02 mm across 1.75mm and 2.85mm spools.
Our proprietary automatic spool winding system applies constant, calibrated tension to prevent overlapping loops, tangles, and binding. Designed specifically for high-speed multi-material automatic material systems (AMS) and direct-drive extruders, Torwell spools unroll smoothly without snagging or layer slippage.
Hygroscopic polymer degradation is completely mitigated prior to export. Every completed spool undergoes high-temp vacuum drying before being wrapped in thick aluminum-laminated or multi-layer PE vacuum bags containing high-capacity desiccant packs, protecting shipments during long ocean freight transits.
Comprehensive technical specifications and printing parameters across Torwell's complete OEM thermoplastic range for procurement engineers and factory sourcing leads.
| Material Grade | Nozzle Temp | Bed Temp | Density (g/cm³) | Tensile Strength | Printability | Key Characteristic & Application |
|---|---|---|---|---|---|---|
| Marble PLA | 190 – 220 °C | 40 – 60 °C | 1.25 | 58 MPa | Very High | Matte marble texture, hidden layer lines, ideal for architecture & decor. |
| Standard PLA | 190 – 220 °C | 0 – 60 °C | 1.24 | 60 MPa | Very High | High accuracy, low odor, foundational material for education & retail. |
| PLA+ (Plus) | 200 – 230 °C | 50 – 60 °C | 1.24 | 65 MPa | Very High | Enhanced toughness and layer adhesion, reduced brittleness. |
| Silk PLA | 200 – 230 °C | 50 – 60 °C | 1.23 | 54 MPa | High | High gloss, silky metallic sheen, ideal for gifts, vases & figures. |
| PETG | 230 – 250 °C | 70 – 80 °C | 1.27 | 50 MPa | High | Chemical resistance, mechanical toughness, clear transparency options. |
| ABS | 230 – 260 °C | 90 – 110 °C | 1.04 | 43 MPa | Medium | Impact strength, heat resistance, suitable for automotive & tool housings. |
| ASA | 240 – 260 °C | 90 – 110 °C | 1.07 | 45 MPa | Medium | UV-stable, weather-resistant, excellent for long-term outdoor fixtures. |
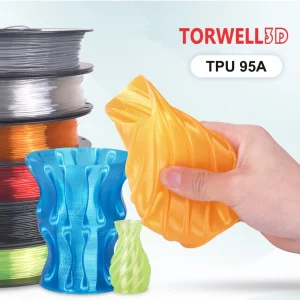
| TPU 95A | 210 – 230 °C | 30 – 60 °C | 1.21 | 35 MPa | Medium | Flexible elastomer, high abrasion resistance, gaskets & soft-touch parts. |
| PC (Polycarbonate) | 260 – 300 °C | 100 – 120 °C | 1.20 | 72 MPa | Advanced | Extreme heat deflection and impact resistance for engineering end-use. |
| Carbon Fiber PLA | 210 – 230 °C | 50 – 60 °C | 1.29 | 75 MPa | High | Chopped carbon fiber composite, high structural rigidity, ultra-lightweight. |
As FDM printing technology accelerates toward ultra-high speed printing, material science must evolve. Explore Torwell's R&D roadmap for next-generation Marble PLA formulations.
Modern 3D printers operate at speeds exceeding 300 mm/s to 600 mm/s. Torwell’s latest Marble PLA chemistry incorporates melt-thinning flow promoters that lower high-shear viscosity, allowing rapid volumetric extrusion without nozzle backpressure buildup or speckle degradation.
Expanding beyond traditional white-and-black marble, advanced compounding facilities now produce multi-tone stone variants including Granite Grey, Sandstone Beige, Obsidian Black, and Emerald Jade Marble, empowering architects with broader material palettes.
Sustainability mandates drive the integration of upcycled organic micro-fillers, such as recycled oyster shell powder and calcined agricultural minerals, replacing synthetic additives to achieve 100% bio-based, industrial-compostable marble filaments.
Next-gen formulations alter surface energy levels post-extrusion, generating microscopic surface roughness that completely eliminates plastic sheen, yielding a cold, tactile texture remarkably close to authentic natural cut stone.
Partnering with international distributors, Amazon brand owners, and regional print farm networks to deliver turnkey private-label manufacturing solutions.
We provide comprehensive private label customization including branded die-cut outer boxes, custom spool label stickers, customized barcode printing, and moisture-proof foil vacuum bag branding tailored to your market specs.
Choose between recyclable eco-friendly cardboard spools or high-durability plastic spools in multiple weight formats: 250g mini spools, standard 1kg retail spools, or industrial 3kg and 5kg bulk spools designed for high-capacity continuous printing.
All Torwell filaments are shipped with full technical data sheets (TDS), safety data sheets (SDS), and certification compliance for global distribution, including RoHS, REACH, and ISO9001 factory documentation.
In-depth technical answers addressing common procurement questions, material dynamics, nozzle requirements, and manufacturing capabilities.
Explore additional high-demand filament grades available directly from Torwell’s automated extrusion manufacturing plant.