Direct from our 2,500 m² automated extrusion plant. Lab-verified batches engineered for consistent viscosity, zero micro-voids, and smooth high-speed feeding across enterprise print farms.

An executive analysis of global thermoplastic procurement shifts, high-speed FDM printer adoption, and total cost of ownership (TCO) optimization for modern print farms and regional distributors.
The global 3D printing filament market is undergoing a structural paradigm shift driven by high-speed CoreXY 3D printers (e.g., Bambu Lab, Creality K1, Voron, Prusa MK4) operating at print speeds from 250 mm/s to 600 mm/s. Traditional PLA formulations fail under high volumetric flow rates due to uneven thermal conductivity and shear-thinning instability. Modern B2B procurement demands optimized polymer melt flow index (MFI) to prevent under-extrusion and heat creep jams.
For enterprise print farms operating hundreds of FDM machines 24/7, filament failure rates directly correlate with operational profitability. Filament diameter drift exceeding ±0.03mm leads to clogging, erratic layer height deposition, and machine downtime. Sourcing directly from certified PLA factories with inline dual-axis laser micrometer monitoring guarantees continuous un-attended operation and predictable unit economics.
Polylactic Acid (PLA) remains the dominant eco-responsible thermoplastic in additive manufacturing. Synthesized from fermented plant starch (corn dextrose or sugarcane), high-purity PLA offers a bio-based carbon footprint 68% lower than petro-chemical polymers like ABS. Global enterprise buyers leverage PLA to fulfill scope 3 carbon reduction quotas and satisfy stringent EU bio-plastic directives without compromising mechanical performance.
Deep polymer engineering insights: Synthesizing virgin high-purity resin, managing melt flow behavior, controlling stereocomplex crystal morphology, and eliminating thermal degradation.
At the molecular level, Polylactic Acid performance depends on the ratio of L-lactide to D-lactide enantiomers. Standard commercial PLA grades utilize raw resin (such as NatureWorks Ingeo™ series) with D-lactide content controlled below 1.5% to ensure rapid crystallization kinetics. Higher D-lactide content suppresses polymer crystallinity, turning the material amorphous and reducing heat deflection temperatures (HDT).
Torwell Technologies formulates virgin resin with specialized nucleating agents and impact modifiers. This optimizes the melt-crystallization phase during extrusion, enabling higher tensile strength (60–65 MPa) and superior interlayer bonding ($E_{11}$ flexural modulus) during fast FDM deposition cooling cycles.
Extrusion consistency requires rigorous thermal and physical regulation. Our automated production lines employ closed-loop dual-axis laser micrometers operating at 500 Hz sampling rates. The digital feedback system instantly modulates haul-off capstan speed and melt pump RPM to maintain diameter precision within a strict ±0.02 mm margin.
Real-time ovality calculation ($D_{max} - D_{min}$) prevents oval cross-sections, guaranteeing smooth, unhindered passages through reverse-Bowden tubes and multi-material switching systems (AMS).
Ensuring flawless thermal melting, high volumetric extrusion rates ($Q_{max} > 32 \text{ mm}^3/\text{s}$), and automatic spool feeder (AMS) compatibility for automated mass production.
Standard PLA exhibits non-Newtonian fluid resistance that stalls high-speed printing. Torwell's high-speed PLA formulation incorporates internal lubricants and chain-extenders that decrease melt viscosity at high shear rates ($10^3 \text{ s}^{-1}$). This enables stable volumetric flow rates up to 32 mm³/s at 220°C without nozzle pressure buildup or gear slipping.
Spool tangling causes instant printing failure. Our automated winding stations feature servo-driven tension controllers and continuous traverse pitch adjustment. Every roll is wound layer-by-layer with strict edge clearance to guarantee smooth payout in enclosed Automatic Material Systems (AMS) and multi-spool hub setups.
By optimizing raw polymer molecular weight distribution ($M_w/M_n$), Torwell PLA achieves a razor-sharp thermal melting window. The material solidifies rapidly upon exiting the nozzle fan cooling zone, minimizing stringing, oozing, and bridging distortion over wide geometric spans.
Established in 2011, operating a 2,500 m² state-of-the-art facility with 6 automated extrusion lines. Turnkey private label solutions for global brands and regional distributors.
Our specialized extrusion lines run 24/7 under HEPA ambient air filtration and precise temperature-profiled screws, producing over 50,000 to 60,000 kg of high-quality filament monthly.
Custom color development with precise spectrophotometer verification. We match custom Pantone codes or physical color plaques within 7 to 10 business days.
End-to-end custom branding: customized cardboard or plastic spools, branded foil vacuum bags, high-grade retail display cartons, and automated barcode/QR labeling.
Every production batch undergoes automated melt index testing, moisture analysis, tensiometer pull tests (ISO 527), and continuous 48-hour printability trial runs.
All Torwell materials are fully compliant with international environmental and chemical safety standards, backed by third-party SGS laboratory certification.
EU Directive 2011/65/EU Free of heavy metals & lead.
EC 1907/2006 SVHC candidate list tested.
Food Contact Safe raw resin formulations.
Approved for toy manufacturing & children products.
| Material Category | Extrusion Temp | Bed Temp | Density (g/cm³) | Tensile Strength | Flexural Modulus | Primary Industrial Application |
|---|---|---|---|---|---|---|
| Standard PLA | 190 – 220 °C | 0 – 60 °C | 1.24 g/cm³ | 62 MPa | 3,800 MPa | Rapid Prototyping, Education, Consumer Models |
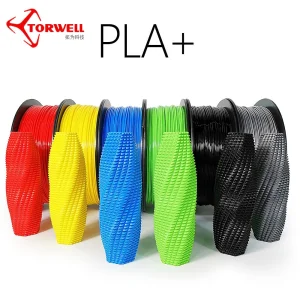
| PLA+ Pro | 200 – 230 °C | 50 – 60 °C | 1.25 g/cm³ | 65 MPa | 3,600 MPa | Functional Parts, Enclosures, Jigs & Fixtures |
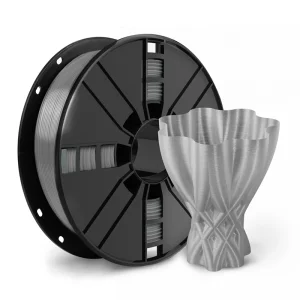
| Silk PLA | 200 – 230 °C | 50 – 60 °C | 1.23 g/cm³ | 56 MPa | 3,200 MPa | Display Models, Aesthetics, Cosplay, Giftware |
| PLA Carbon Fiber | 215 – 240 °C | 50 – 70 °C | 1.29 g/cm³ | 72 MPa | 4,900 MPa | Drone Frames, Automotive Fixtures, Tooling |
| PETG Engineering | 230 – 250 °C | 70 – 80 °C | 1.27 g/cm³ | 50 MPa | 2,100 MPa | Chemical Containers, Outdoor Enclosures |
| ABS Industrial | 230 – 260 °C | 90 – 110 °C | 1.05 g/cm³ | 43 MPa | 2,300 MPa | Automotive Trim, Snap-fit Assemblies, Housings |
| TPU Flexible 95A | 210 – 230 °C | 30 – 60 °C | 1.21 g/cm³ | 35 MPa (Elongation > 450%) | N/A | Gaskets, Seals, Footwear, Protective Dampeners |
| PC Polycarbonate | 260 – 300 °C | 100 – 120 °C | 1.20 g/cm³ | 70 MPa | 2,400 MPa | High Heat Structural Components, Optics Covers |
Ensuring zero moisture degradation during long-distance ocean freight and advancing next-generation sustainable polymer technology.
PLA polymer is inherently hygroscopic. Hydrolysis degrades polymer chain length when exposed to ambient moisture. Torwell employs a multi-tier protective packaging system: inline thermal desiccation drying prior to spooling, followed by immediate vacuum sealing in thick aluminum composite foil bags with active silica gel packs.
Exporting to over 75 countries across North America, Europe, South America, and Asia-Pacific. We provide complete export documentation including HS Code classification (3916.90.00), Certificate of Origin (CO), MSDS, and DDP/FOB/CIF international shipping terms.
Our material engineering division is currently scaling next-generation additive materials: Flame Retardant PLA (UL94 V-0 certification), Bio-based High Heat PLA (HDT > 105°C post-annealed), and fully ocean-degradable PHA/PLA bio-composites.
High-performance material selection for wholesale buyers, OEM private label customers, and high-volume print farms.
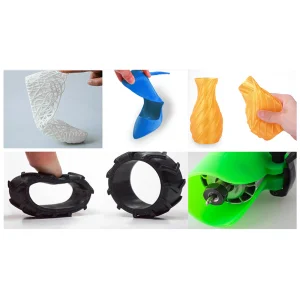


Direct answers to critical procurement, technical specification, OEM branding, and freight logistics questions asked by enterprise buyers.
Ready to optimize your supply chain, enhance print farm reliability, or launch your private label filament brand? Contact our enterprise engineering team today for factory direct quotations and physical material samples.
