Direct factory supply engineered to ±0.02 mm tolerance for consistent extrusion performance.

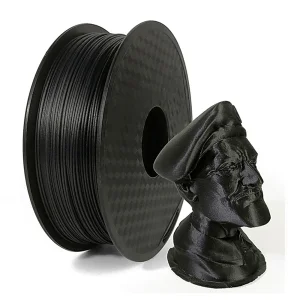
Understanding the chemical engineering behind particle-suspended aesthetic thermopolymers.
In fused deposition modeling (FDM), standard monofilaments yield uniform monochromatic surfaces that frequently accent layer lines and internal toolpath boundaries. Marble PLA 1.75mm filament represents a specialized class of modified biopolymers engineered to produce authentic, stone-like aesthetic textures directly out of the hotend—eliminating the need for tedious manual post-processing, priming, or painting.
Achieving a convincing marble appearance requires compounding premium Polylactic Acid (PLA) virgin resin with micronized, high-thermal-stability organic flecks and non-abrasive inorganic mineral micro-particles. Unlike abrasive stone-fill composite filaments (such as real marble powder or gypsum suspensions) which rapidly erode brass extruder nozzles and cause severe melt-flow turbulence, modern Chinese manufacturing innovations utilize advanced polymer compounding. This approach embeds thermal-resistant particulate flecks into the PLA matrix without compromising melt flow index (MFI) or increasing shear friction.
Maintains a Melt Flow Index (MFI) of 6–10 g/10min (210°C/2.16kg), ensuring consistent volumetric flow rates up to 300 mm/s on modern high-speed coreXY platforms.
Formulated with soft, heat-resistant particulate flecks that preserve nozzle orifice geometry, extending brass nozzle operational lifespans by up to 400% vs. real ceramic fillers.
Randomized speckle distribution visually scatters incident light, effectively masking 0.12mm–0.28mm layer lines to yield a smooth, matte stone-like surface finish.
The primary technical challenge during Marble PLA 1.75 mm extrusion is preventing particulate agglomeration. If speckle additives clump inside the melt zone, local pressure spikes occur, causing filament diameter swelling (exceeding +0.05 mm) and severe nozzle blockages. Top-tier Chinese manufacturers employ high-shear twin-screw extruders operating under closed-loop nitrogen gas shielding. This process homogenizes the polymer dispersion while preventing thermo-oxidative degradation of the base PLA polymer chain.
Global procurement metrics, supply chain resilience, and industrial cluster synergies in additive manufacturing material production.
China has solidified its position as the global center for additive manufacturing material supply, producing over 70% of the world's commercial FDM printer filaments. Sourcing Marble PLA 1.75mm directly from established OEM/ODM manufacturers in China provides enterprise procurement officers, brand owners, and distributor networks with decisive competitive advantages across quality, cost scalability, and custom formulation speed.
Leading Chinese extrusion facilities operate continuous dual-axis or quad-axis laser diameter measurement systems. Operating at 500 Hz sampling rates, these systems auto-adjust capstan pulling speeds in real time to guarantee a true dimensional tolerance of ±0.02 mm across full 1,000-meter spool runs.
Direct supply contracts with primary PLA resin synthesizers (such as NatureWorks Ingeo, Total Corbion, and Huarun) grant Chinese factories preferred pricing on high-purity medical/food-grade PLA bases. These cost efficiencies are directly passed on to OEM partners.
Hygroscopic polymer protection is vital. Chinese factories utilize vacuum-assisted inline dehumidifying hoppers (reducing moisture levels to < 200 ppm) paired with robotic neat-winding hardware to eliminate overlapping loops, tangles, and atmospheric moisture absorption.
B2B buyers can request custom marble shades—ranging from standard Carrara White and Granite Grey to Obsidian Black, Terracotta Sandstone, and Jade Green Marble—with turnkey masterbatch matching within 7 to 10 working days.
Furthermore, Chinese factory infrastructures support complete private-label white-glove packaging services: custom die-cut inner boxes, eco-friendly moisture-proof cardboard spools, specialized desiccant packs, high-barrier vacuum seal packaging, and serialized QR-code tracking for batch transparency.
Quantitative empirical benchmarking of Marble PLA 1.75mm against standard 3D printing polymers.
To assist material engineers and procurement managers in selecting the ideal material for specific end-use applications, the table below outlines the mechanical, thermal, and physical characteristics of China-manufactured Marble PLA 1.75mm alongside standard printing thermoplastics.
| Mechanical / Thermal Property | Marble PLA 1.75mm | Standard PLA | Tough PLA / PLA+ | PETG | ABS (Engineering) |
|---|---|---|---|---|---|
| Density (g/cm³) | 1.25 – 1.28 | 1.24 | 1.23 – 1.25 | 1.27 | 1.04 |
| Tensile Strength (MPa) | 52 – 58 | 55 – 65 | 60 – 68 | 48 – 52 | 40 – 45 |
| Flexural Modulus (GPa) | 3.1 – 3.4 | 3.2 – 3.8 | 2.8 – 3.2 | 2.1 – 2.4 | 2.0 – 2.3 |
| Charpy Impact Strength (kJ/m²) | 4.8 – 5.5 | 5.0 – 6.0 | 8.5 – 12.0 | 6.5 – 8.0 | 15.0 – 20.0 |
| Heat Deflection Temp (HDT @ 0.45 MPa) | 55°C – 58°C | 56°C – 60°C | 58°C – 62°C | 68°C – 72°C | 85°C – 95°C |
| Optimal Printing Temperature | 200°C – 220°C | 190°C – 210°C | 205°C – 225°C | 230°C – 250°C | 240°C – 260°C |
| Recommended Bed Temperature | 45°C – 60°C | 45°C – 60°C | 50°C – 65°C | 70°C – 80°C | 90°C – 110°C |
| Surface Aesthetic Finish | Matte Speckled Stone | Glossy Monochromatic | Satin Monochromatic | High Gloss Semi-Clear | Matte / Satin (Solvent Treatable) |
*Note: Data derived from standardized ISO 527 tensile and ISO 179 impact tests performed on 100% infill 3D printed test specimens extruded at 210°C, nozzle 0.4mm, layer height 0.2mm.
From architectural scale modeling to luxury product prototyping: Where Marble PLA delivers maximum ROI.
Architectural firms and urban planning agencies rely heavily on Marble PLA to produce high-precision scale models of building facades, structural columns, and urban master plans. The natural stone texture provides a realistic, premium finish that simulates carved Carrara marble or limestone without requiring manual painting or post-assembly labor.
Cultural institutions, heritage preservation teams, and digital sculptors utilize 3D scanning paired with Marble PLA 1.75mm printing to replicate classical Roman and Greek sculptures, museum display replicas, and architectural restoration moldings with high tactile realism.
Industrial product designers leverage Marble PLA for luxury home decor items—including organic-shaped vases, acoustic speaker enclosures, modern lighting fixtures, decorative containers, and boutique retail display stands—commanding higher retail margins than standard plastic goods.
Technical tuning for Bambu Lab, Creality K1, Voron 2.4, and industrial multi-filament setups (AMS/KCM).
The additive manufacturing industry has undergone a rapid paradigm shift toward ultra-high-speed printing, with modern FDM platforms regularly operating at print speeds between 250 mm/s and 500 mm/s with accelerations exceeding 10,000 mm/s². Standard composite filaments often fail under these extreme shear conditions due to improper melt enthalpy or nozzle clogging.
China's leading Marble PLA 1.75mm factory formulations are specifically optimized for high-speed motion systems, incorporating thermal flow enhancers and narrow molecular weight distribution (MWD) polymers.
Streamlining global B2B procurement, customized brand packaging, and international freight compliance.
For international distributors, Amazon top-sellers, and enterprise procurement managers, securing a reliable supply chain partner in China requires looking beyond base material price. Quality assurance protocols, shipping logistics compliance, and customizable branding solutions dictate long-term brand profitability.
Full OEM capabilities: customized spool stickers, branded inner boxes with custom die-cut windows, branded outer master cartons (10 or 12 spools/carton), and integrated QR codes for lot tracing.
All exported Marble PLA 1.75mm filaments comply fully with European Union RoHS Directive 2011/65/EU, REACH (EC 1907/2006), and FDA food-contact safety standards for raw PLA bases.
Optimized palletization strategies maximize container space: a standard 20ft FCL accommodates approx. 10,000 kg (10,000 spools), while a 40ft HQ container holds up to 22,000 kg with heavy-duty moisture-barrier wrapping.
What's next for decorative FDM materials: Bio-composites, multi-gradient co-extrusion, and smart formulations.
As consumer expectations shift toward high-value, functional aesthetic parts, the market for Marble PLA 1.75mm is expanding beyond simple white-and-black speckle patterns. Leading R&D laboratories in China are pioneering next-generation decorative biopolymers designed for demanding architectural and industrial design challenges:
Technical and commercial answers for OEM brands, wholesale buyers, and print farm operators.
Partner with China's leading 3D printing filament manufacturer. Get direct factory pricing, technical data sheets (TDS), and custom masterbatch samples within 5 business days.
Contact Factory Sourcing TeamExplore our full factory catalog of advanced FDM 3D printing materials.